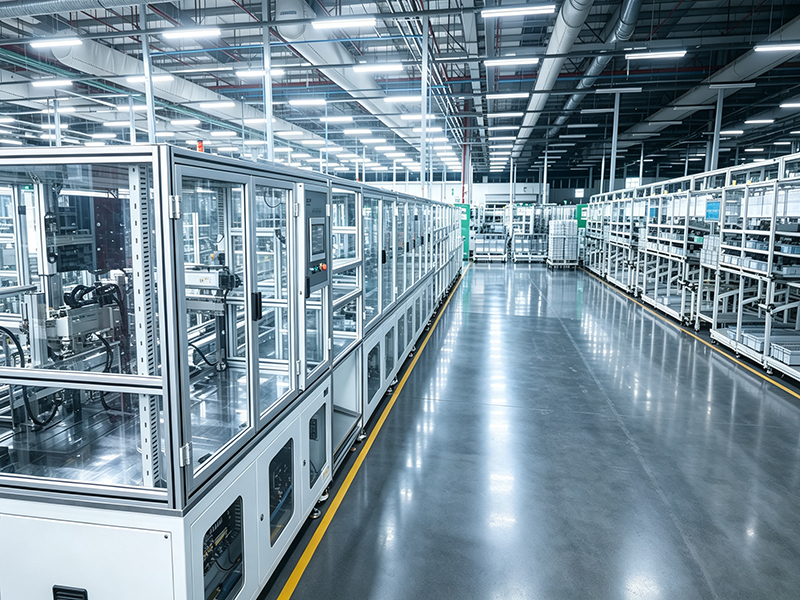
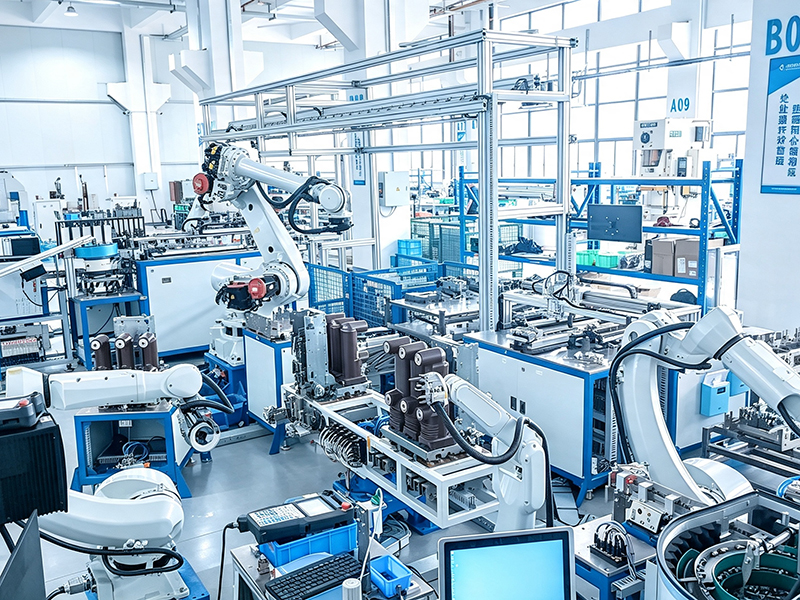
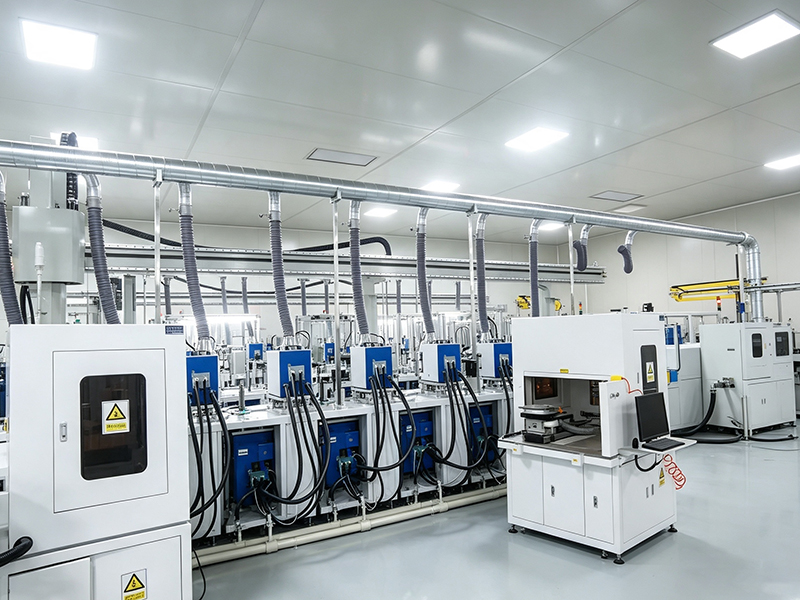
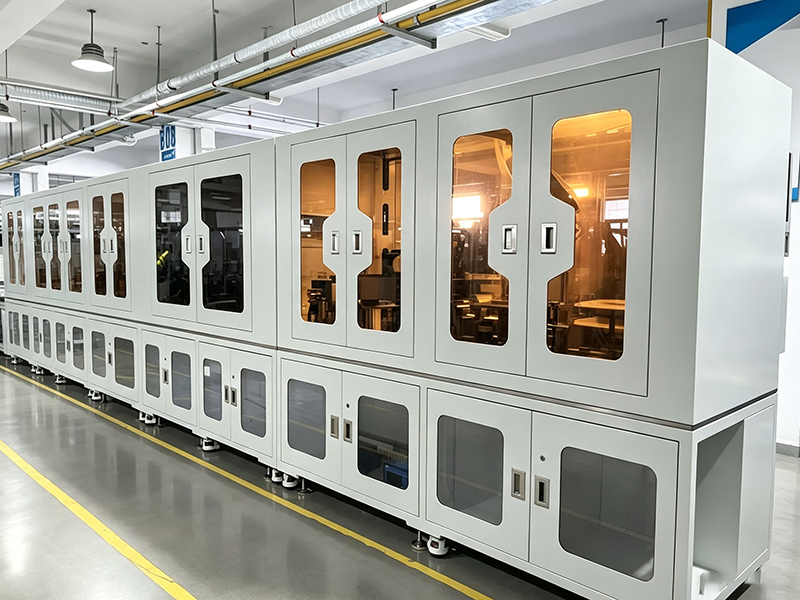
The MCB Automatic Assembly, Testing & Packing Line is a fully automated production line tailored to the MCB series miniature circuit breakers, covering the complete process from part welding, sub-assembly, finished-product testing through packing and warehousing. The equipment can adapt to a variety of customer MCB models — rated currents 20A / 25A / 32A / 40A, poles 1P / 2P / 3P / 4P (sharing the same multi-pole housing), rated voltage 230V.
The line consists of two main sections — Assembly & Welding and Testing & Packing — built around a 65 mm pallet conveyor in a closed-loop layout with counter-clockwise material flow, and matched cycle times between the two halves. Each station is PLC-controlled and operated via HMI; stations are independent and can run standalone. Every station features audible/visual alarms, fault indication and query, with two-tier access (operator / engineer).
A line-level host computer collects production data from every station and exchanges seamlessly with the customer's ERP/MES — providing automatic statistics on real-time output, pass/fail counts, station OEE and full-process traceability. Product changeover is performed by entering the new model code at the packing-line industrial PC; all stations then automatically switch to the corresponding parameters. The system also monitors preventive-maintenance schedules.
The line uses a closed-loop pallet conveyor with counter-clockwise material flow: the Assembly & Welding section (stations 01–09) runs along the lower lane, and the Testing & Packing section (stations 10–19) returns along the upper lane, with both ends automatically linked by the loop. Overall footprint is approximately 44,000 mm × 4,500 mm; frame height 2,000 ± 50 mm; conveyor surface height above floor 850 ± 50 mm; the size of individual frames accounts for factory elevator transport constraints.
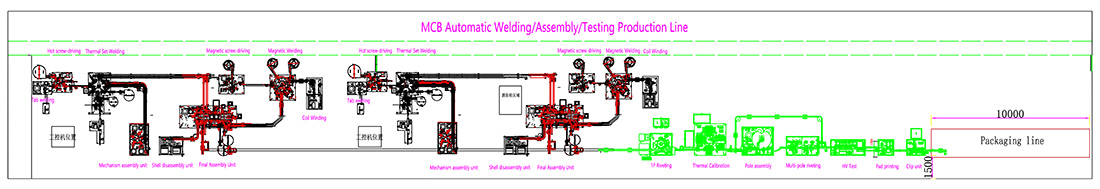
gure 1 — Line Layout · Counter-clockwise material flow
A shell/parts AGV loading interface is provided (automatic tote-box docking, six-axis robot picking, empty totes auto-slide-out). The final-assembly section retains a manual fly-wire assembly station per the technical agreement. Non-conforming products are diverted through an independent channel (buffer ≥ 50 pieces). The host computer sits at the centre of the loop, collecting data from every station and interfacing with ERP/MES. Finished products are output from the auto-carton station.
Across six dimensions — cycle time & capacity, labour-saving automation, process quality, closed-loop testing, informatization, and key configurations — the core advantages of this solution are summarised below.
Whole-line capacity (8 h)
≥ 16,300 poles
Assembly station cycle
< 3 s/pole
Testing & packing station cycle
1.5 s/pole
Assembly line target OEE
85%
Modular Architecture
Independent Operation
Data Integration
ERP/MES Traceability